
丨
English
Views: 0 Author: Site Editor Publish Time: 2026-10-01 Origin: Site


Industrial material handling equipment operates under extreme dynamic loads. These machines endure constant vibration during daily operations. They must also comply strictly with international safety mandates. Consequently, component failure represents a high-liability risk for fleet operators. Original equipment manufacturers face a highly specific engineering problem. Procurement engineers must balance the demand for high tensile strength. They need this structural strength alongside massive impact resistance. Simultaneously, they must maintain manufacturing scalability and control production budgets. This article explores a highly reliable material solution. You will discover why ductile iron serves as the baseline specification. We explain its advantages over grey cast iron and expensive steel forgings. Finally, you will learn how this material optimizes safety-critical drivetrain and structural applications.
Ductile iron provides the high yield strength and impact fatigue resistance necessary for critical load-bearing forklift systems.
Common applications include steering knuckles, axle housings, brake spacers, and mast mounting brackets.
Sourcing custom ductile iron components requires evaluating a foundry's non-destructive testing (NDT) capabilities and metallurgical consistency.
Procuring finished, machined ductile iron parts directly from a single-source foundry reduces supply chain bottlenecks and ensures tolerance compliance.
Ductile iron possesses a highly unique microscopic structure. It features nodular graphite formations rather than flat flakes. Standard grey iron contains these flat graphite flakes. Those flakes act as internal stress points. They encourage cracks to propagate under heavy loads. Nodular graphite prevents this dangerous crack propagation entirely. This microscopic difference grants the material superior tensile strength. It also provides excellent ductility for heavy machinery. Compared to steel forgings, ductile iron offers exceptional vibration damping. It also delivers much better castability for complex geometries.
Tensile Strength: It handles massive pulling forces without fracturing.
Vibration Damping: The graphite nodules absorb operational engine frequencies naturally.
Ductility: It can flex slightly under extreme pressure without snapping.
Castability: Molten ductile iron flows easily into intricate mold cavities.
Forklifts operate in demanding warehouses and rough-terrain environments. These conditions subject vehicle structures to intense cyclic loading. A machine might lift a three-ton pallet fifty times daily. This repetitive action stresses the chassis and lifting mechanisms continuously. Ductile iron handles these intense forces beautifully. It resists fatigue from repetitive motion incredibly well. When operators navigate over uneven loading docks, the chassis absorbs heavy impacts. Ductile iron components survive these sudden shock loads. They deform elastically instead of shattering instantly.
Manufacturers achieve significant economic advantages using this material. Foundries cast complex near-net shapes easily. A near-net shape closely resembles the final desired product. This efficient process reduces raw material waste dramatically. It eliminates the need for excessive rough machining. Furthermore, engineers can design thinner component walls. They maintain the same structural integrity as thicker grey iron parts. This intelligent design strategy lowers the overall vehicle weight. A lighter vehicle consumes less fuel and requires less battery power.
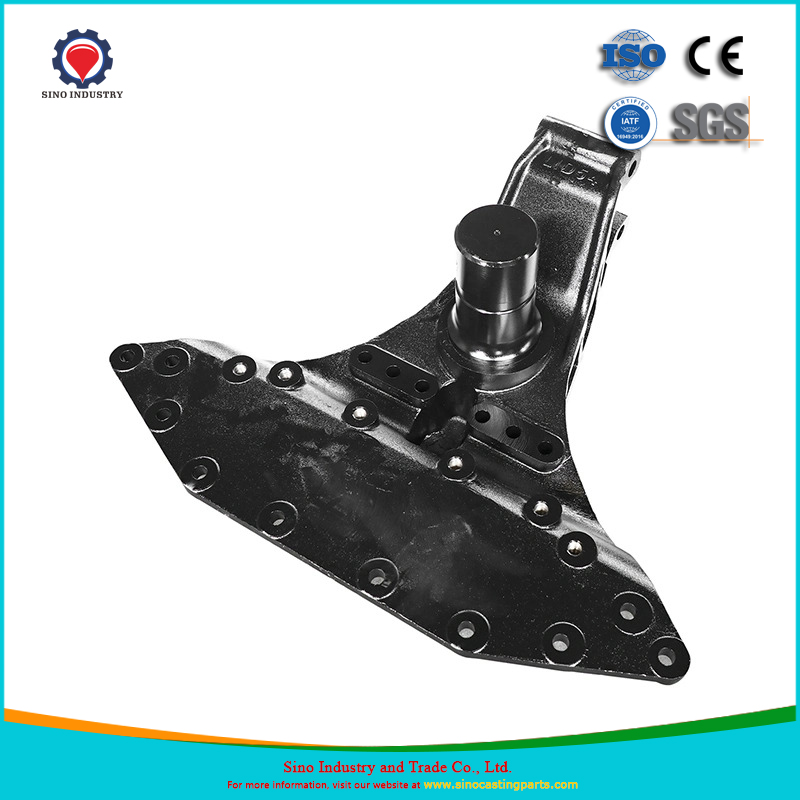
The rear steering mechanism requires massive impact resistance. It must distribute heavy loads evenly across the rear tires. When a forklift carries a maximum payload, the rear axle acts as a crucial counterweight. Material fatigue here risks a total loss of directional control. High-quality ductile iron forklift components excel in this specific application. They resist fatigue and keep operators completely safe. A cracked steering knuckle easily causes catastrophic workplace accidents.
Forklift braking systems generate immense friction and heat. Brake spacers require strong thermal stability to function correctly. They also need strict dimensional accuracy. This precision ensures consistent braking force across the entire axle. It also minimizes dangerous brake fade during repetitive stops. Wheel hubs face similar operational challenges. They endure rotational stress while supporting the vehicle's entire weight. Ductile iron maintains its dimensional stability even under high thermal loads.
Masts hoist asymmetric and maximum-capacity loads high into the air. The mounting brackets require absolute structural rigidity. They must resist severe bending moments constantly. When a heavy load shifts slightly, the carriage experiences sudden torsional stress. Ductile iron provides the stiffness necessary to stabilize the carriage. It prevents the mast from bending dangerously during heavy lifts. These components form the literal backbone of the lifting mechanism.
Internal transmission gearing needs protection from harsh operational vibrations. Hydraulic systems demand highly rigid containment vessels. Ductile iron housings absorb chassis vibrations effectively. They prevent these vibrations from damaging sensitive internal gears. They also prevent fluid leaks by maintaining stiff, unyielding seal faces. A flexing transmission housing quickly destroys internal bearings. Ductile iron ensures the drivetrain remains perfectly aligned.
Ductile Iron Component Analysis
Component Type | Primary Engineering Requirement | Critical Failure Risk Prevented |
|---|---|---|
Steering Knuckles | High impact resistance & fatigue strength | Loss of directional control under load |
Brake Spacers | Thermal stability & dimensional accuracy | Brake fade and uneven stopping force |
Mast Brackets | High rigidity & resistance to bending moments | Mast collapse or dangerous load shifting |
Drivetrain Housings | Vibration damping & pressure containment | Internal gear misalignment and fluid leaks |
Standard catalog parts often fall short of modern engineering requirements. OEMs frequently design specialized attachments for unique industries. They constantly upgrade payload capacities for new heavy-duty models. They also adapt standard chassis designs for narrow-aisle warehouses. These engineering shifts act as major project triggers. They necessitate custom solutions tailored to specific structural stress points. You cannot rely on standard castings when designing proprietary lifting geometries.
Transitioning requires a deeply collaborative engineering process. Foundry engineers must optimize the tooling design first. They run advanced flow simulations using specialized software. These digital simulations ensure molten metal fills the mold cavity perfectly. They identify potential cold shuts or porosity risks before pouring. Foundries then pour custom ductile iron components tailored exactly to proprietary OEM geometries. This collaboration eliminates costly redesigns later.
CAD Review: Engineers analyze the 3D models for castability issues.
Flow Simulation: Software predicts how molten iron will behave inside the mold.
Pattern Creation: Tooling experts craft accurate patterns from aluminum or resin.
Sample Pouring: The foundry produces initial prototypes for physical testing.
Lead times demand careful production planning. Pattern making typically takes several weeks to complete. Foundries must conduct a rigorous First-Article Inspection (FAI). This comprehensive checking validates the physical prototype against original drawings. Inspectors verify dimensions, material properties, and surface finishes. Only after full FAI approval does the transition begin. The foundry then moves smoothly into high-volume production. Planning for these realities prevents unexpected supply chain delays.
A raw casting rarely fits straight into a final vehicle assembly. Moving parts demand extremely strict dimensional accuracy. Steering linkages and mast assemblies require exact fits to function. Without this precision, mechanical linkages bind. Slower moving parts might suffer from severe friction. Unmachined mating surfaces cause rapid mechanical wear. Precision machining transforms a strong raw casting into a functional mechanical component.
CNC machining achieves these necessary operational tolerances reliably. Strict surface finishes are an absolute operational necessity. They prevent premature wear on expensive mating components. They protect vulnerable hydraulic seals from rapid abrasion. A rough surface finish on a hydraulic cylinder mount ruins seals quickly. Tight CNC tolerances ensure bolts align perfectly during final assembly. This precision prevents mechanics from forcing parts together on the assembly line.
Fragmented supply chains increase quality control risks significantly. Shipping raw castings to a separate machine shop adds logistical complexity. Smart OEMs consolidate their sourcing strategies. They buy fully machined ductile iron parts directly from integrated foundries. This strategic approach guarantees single-point accountability. If a defect occurs, the foundry handles it completely. It reduces logistical bottlenecks and streamlines the entire procurement process.
Quality control starts with absolute material verification. Foundries must document their heat lots meticulously. They should conduct regular spectrographic analysis on every pour. This analysis ensures the chemical composition matches the required grade perfectly. Verifiable material certifications are entirely mandatory. These documents prove legal compliance with national and international forklift safety standards. Without proper traceability, you cannot guarantee component reliability.
Visual surface inspections are never enough for safety-critical parts. Subsurface defects cause catastrophic mechanical failures in the field. Foundries must use Non-Destructive Testing (NDT) protocols. Ultrasonic testing checks for internal voids hidden deep inside the metal. Magnetic particle inspection reveals microscopic surface cracks invisible to the naked eye. X-ray protocols identify hidden porosity or sand inclusions. Good foundries identify these flaws before parts reach your assembly line.
OEM production demands fluctuate constantly throughout the year. A reliable casting supplier adapts quickly to these changes. You must assess their capacity for ongoing tooling maintenance. Patterns wear out and require repair or replacement. The foundry must manage varying production runs smoothly. Delivering consistent quality across both low and high volumes is absolutely essential. A good partner grows their capacity alongside your business.
Finding the right casting partner requires a highly systematic approach. Request comprehensive technical audits from your shortlisted suppliers. Review their past material handling manufacturing case studies. Understand how they solved similar engineering challenges previously. Finally, initiate a detailed Request for Quote (RFQ). Base your final decision on long-term supplier reliability and integrated production capabilities rather than unit price alone.
Selecting the right casting material directly impacts overall forklift safety. It extends equipment lifespan significantly and reduces unexpected maintenance downtime. Choosing an experienced manufacturing partner directly reduces future warranty claims. Ductile iron remains the superior choice for critical load-bearing applications. It simply outperforms standard grey iron and expensive steel alternatives. Engineers and procurement teams should take proactive steps today. Submit your complex CAD files to a trusted foundry partner. Request a thorough manufacturability review and structural analysis. Ask for exact material grade recommendations tailored specifically to your vehicle's payload requirements. Consolidate your supply chain to secure higher quality control and faster assembly times.
A: The primary difference lies in the microscopic graphite structure. Standard grey iron contains graphite flakes, making the material brittle under tension. Ductile iron features nodular (spherical) graphite. These nodules prevent internal crack propagation. This unique structure grants the material high tensile strength, excellent ductility, and the massive impact resistance essential for heavy material handling equipment.
A: Forklift manufacturers frequently specify standard grades like ASTM A536 65-45-12 or 80-55-06. The 65-45-12 grade offers maximum ductility and high impact resistance, perfect for steering components. The 80-55-06 grade provides higher yield strength and better wear resistance, making it ideal for heavily loaded drivetrain parts. Both grades balance strength and machinability beautifully.
A: Welding ductile iron poses severe metallurgical challenges and immense safety risks. High heat alters the nodular graphite structure permanently. This creates brittle micro-zones highly prone to catastrophic failure. Due to strict industry safety regulations, you should never repair load-bearing forklift components. You must always replace damaged structural parts with new, certified castings.
A: Developing new tooling typically takes four to eight weeks, depending heavily on part complexity. This timeline includes 3D pattern creation, gating design, and digital flow simulation. Pouring and inspecting initial samples adds another two to four weeks. Once the First-Article Inspection (FAI) is officially approved, high-volume production ramp-up usually begins immediately.


